Saturday, 3 December 2016

DESIGN OF SHAFTS

PURE TORSION

when the shaft is subjected to pure torsional load,the diameter of the shaft may be obtained by using torsion equation


                              τ = T r / J

where,
τ=  torsional shear stress
T= torque acting upon the shaft
r = radial distance of the outermost fibre
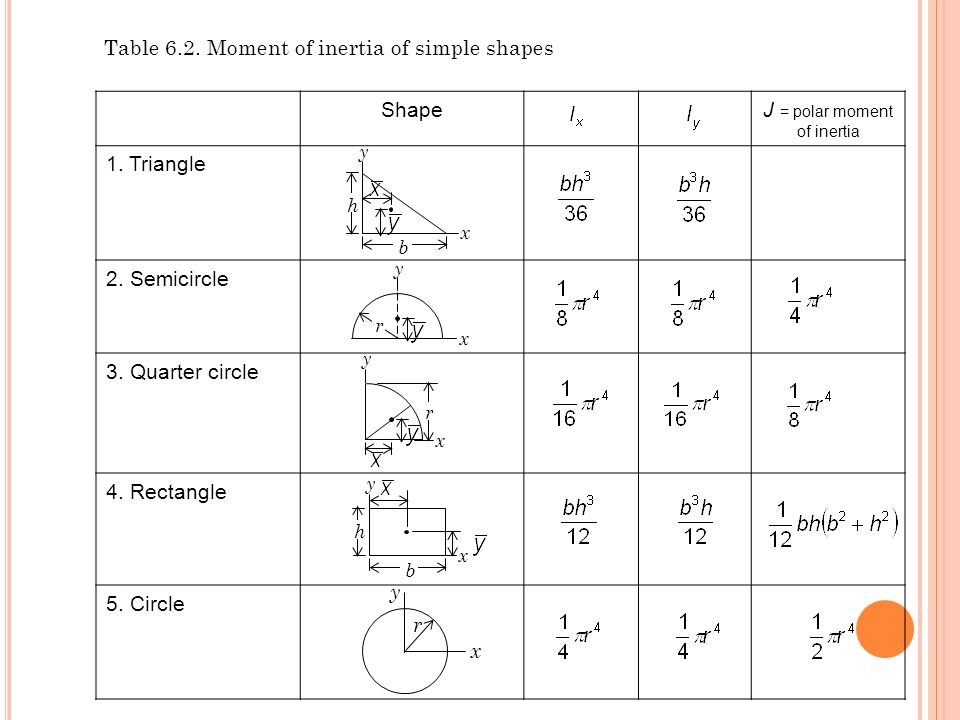
J = polar moment of inertia

Note:-

The "Polar Moment of Inertia of an Area" is a measure of a beam's ability to resist torsion. The "Polar Moment of Inertia" is defined with respect to an axis perpendicular to the area considered. It is analogous to the "Area Moment of Inertia" - which characterizes a beam's ability to resist bending - required to predict deflection and stress in a beam.

"Polar Moment of Inertia of an Area" is also called "Polar Moment of Inertia", "Second Moment of Area", "Area Moment of Inertia", "Polar Moment of Area" or "Second Area Moment".


        τ=16T/πd^3

∵      J= (π/32)*d^4

         r=d/2


FOR HOLLOW SHAFT JUST REPLACE D^4 WITH [d⁴₀-dᵢ⁴]

where ,

d⁴₀ =outer dia
dᵢ⁴ = inner dia

Friday, 2 December 2016

Calculating the section modulus

To calculate the section modulus, the following formula applies:

An equation: Z = I /y.  

where I = moment of inertia,
           y = distance from centroid to top or bottom edge of the rectangle, here d/ 2. 

For symmetrical sections the value of Z is the same above or below the centroid.

For asymmetrical sections, two values are found: Z max and Z min.

To calculate the value of Z for a simple symmetrical shape such as a rectangle:

An equation: Zxx = I xx/y.  where An equation: Ixx = bd3/12 mm4.

and y=d/2

This gives the formula for  Z = bd2/6 mm3.


Thursday, 24 November 2016

PLASTIC EXTRUSION AND MOULDING

EXTRUSION MOULDING
Extrusion is a manufacturing process used to make pipes, hoses, drinking straws, curtain tracks, rods,and fiber. The granules melt into a liquid which is forced through a die, forming a long 'tube like' shape.The shape of the die determines the shape of the tube.The extrusion is then cooled and forms a solid shape.The tube may be printed upon,and cut at equal intervals.The pieces may be rolled for storage or packed together.Shapes that can result from extrusion include T-sections,U-sections,square sections,I-sections,L-sections and circular sections.One of the most famous products of extrusion moulding is the optical fiber cable.
Everyday examples of extrusion can be seen when toothpaste is squeezed out of a tube, icing is pushed out of an icing bag and "Play do" shapes are made. Extrusion moulding of plastics is used to make any long shape that has a constant cross section. Pipes, gutters, window sections and decorative trims can all be made using the process.,

Typical extrusion material-
• PVC (polyvinylchloride), 
• LDPE (low-density polyethylene, or polythene), 
• HDPE (high density polyethylene) and 
• PP (polypropylene) 

Thermoplastics are pliable when they are heated but form a rigid shape once cooled. Perhaps most common plastic extruded is PVC. Hard, "unplasticised" PVC can be used in pipes for water, sewage and gas.


Working principle
The extrusion process begins with the plastic polymer in a granule or powder form. A funnel, or hopper, feeds this into the heating chamber of the extruder. The polymer melts as it is heated to temperatures typically above 200ºC
 Once molten, a screw-mechanism pushes the melted polymer through the shaped "die head" which forms the plastic into shape. As it leaves the extruder, the plastic is cooled by water or air to give the final form. Flexible products, like tubing, may be coiled whilst rigid plastics, such as window-frame sections, will be cut to length.

Parts of plastic moulding machine-


Hopper
The hopper is a large funnel that holds the raw plastic in either granular or pellet form. The hopper sends a continuous stream of raw plastic into the heating barrel of the extrusion machine.


Heated Barrel
The heated barrel of a plastic extrusion machine is a long, horizontal cylinder. The cylinder is heated internally through the use of a heating jacket. As the plastic is fed into the cylinder by the hopper, the plastic melts from the heat 

Die and Mandrel
 A water-cooled die is located at the end of the heated barrel. The intended shape of the plastic is cut into the die. Water passes along the metal die to cool the plastic as it passes and harden it into shape. A mandrel may also be located after the die to produce a hollow shape.
Screw design:-


Most screws have these three zones:
• Feed zone (also called the solids conveying zone): this zone feeds the resin into the extruder, and the channel depth is usually the same throughout the zone.
• Melting zone (also called the transition or compression zone): most of the polymer is melted in this section, and the channel depth gets progressively smaller.
• Metering zone (also called the melt conveying zone): this zone melts the last particles and mixes to a uniform temperature and composition. Like the feed zone, the channel depth is constant throughout this zone.


Compound extrusions
Compounding extrusion is a process that mixes one or more polymers with additives to give plastic compounds. The feeds may be pellets, powder and/or liquids, but the product is usually in pellet form, to be used in other plastic-forming processes such as extrusion and injection molding. As with traditional extrusion, there is a wide range in machine sizes depending on application and desired throughput. While either single- or double-screw extruders may be used in traditional extrusion, the necessity of adequate mixing in compounding extrusion makes twin-screw extruders all but mandatory
Application:-
• Insulated coating for wires and cables.
• Monofilament: for rope, bristles and synthetic textile fibres.
• Flat plastic sheets for signs, refrigerator interiors, glazing and lighting applications.
• Pipes and tubing used for hoses, water, gas, sewers and drains.

 Advantages of Plastic Extrusion
      3 of the major advantages of plastic extrusion are as follows.
• Low Cost: Compared to other molding processes, plastic extrusion molding has a low cost and is more efficient. The extrusion molding process uses thermoplastics and they undergo repeatedly melting and hardening, this allows the waste to be reused rather than be discarded. Raw material and disposal costs are lowered. 
• Better Flexibility: Extrusion molding will provide considerable flexibility in the products being manufactured with a consistent cross section. As long as the cross section stays the same, the extrusion molding can produce complex shapes
• After Extrusion Alterations: Plastics remain hot when they are removed from the extruder and this allows for post-extrusion manipulations. Many manufacturers will take advantages of this and use a variety of roller, shoes and dies to change the shape of the plastic as needed.

 Disadvantages of Plastic Extrusion
Plastic extrusion has also some disadvantages.
• Expansion: Once the hot plastic is removed from the extruder it will many times expand. This is called die swell. It is problematic to try and predict the exact degree of expansion. Because it is hard to predict the exact expansion, manufacturers often accept significant levels of deviation from the dimensions of the product.
• Product Limitations: Extrusion plastic molding does place limits of the types of products that can be manufactured. There are alternatives that require an investment in a different type of extrusion equipment.

Sunday, 13 November 2016

DIFFERENCE BETWEEN FRANCES AND KAPLAN TURBINE


1. Type of Turbine
      France Turbine is radially in ward or mixed flow Turbine
      Kaplan Turbine is partially axial flow


2. Disposition of shafts

      France Turbine disposition of shaft is in vertical or horizontal direction
      Kaplan Turbine disposition of shaft is only in vertical direction


3. Number of vanes

     France Turbine has very large number of blades 16 to 24
     Kaplan Turbine has very small number of blades 3 to 8


4. Adjustment of runner vanes 

     France Turbine Runner vanes are not adjustable
     Kaplan Turbine Runner vanes are adjustable

5. Resistance to over come

     France Turbine very large resistances have to be over come
     Kaplan Turbine very less resistances have to be over come
6. Head

     France Turbine medium head is required
     Kaplan Turbine very low head is required
7. Flow Rate

     France Turbine medium flow rate is required
     Kaplan Turbine very large flow rate is required
8. Specific Speed

     France Turbine 50 to 250
     Kaplan Turbine 250 to 850
9. Type of generator

     France Turbine regular generator is required
     Kaplan Turbine heavy duty generator is required

Monday, 31 October 2016

CHANGING LOCATION IN TINDER WITHOUT PAYING FOR IT

YES U HEARD IT RIGHT now you can fake your location in tinder app without paying for it thus you will have the power to explore and find a perfect match for you sitting at home 

Requirements:-

1. fake GPS app(play store link)
2. An android mobile phone
3. Data pack 

 NOTE:- This tutorial will not work with a wifi connection.

STEP 1 -  Turn on your mobile data 2G,3G or 4G


STEP 2- Download the above fake GPS app and install it on your phone and open it now you will see a search box there search your desired location and then tap the green circular button having white triangle inside it located at the lower right end of your phone screen.
now the app will automatically close showing a notification with a pause button the latitude and longitude of that fake location(we don't have to do anything with this ).

STEP 3- Now open your tinder app now it will ask you to turn your wifi on press ok and allow it 

STEP 4- Now a home screen with tinder default layout will open written as 'finding people near you'

Hola now tinder will search people near your fake location and you will find people around that fake location


How to change the location 2nd time??
After using first time above method  to change your location again turn off your mobile data and force stop both tinder app and fake gps app and clear cache now repeat the above MENTIONED steps enjoyyy 


Saturday, 24 September 2016

DIFFERENT FORMS OF IRON BASED ON CARBON CONTENT


HERE ARE SOME BASIC BUT VERY IMPORTANT TERMS EASILY EXPLAINED FOR YOU RELATED TO PIG IRON,CAST IRON,WROUGHT IRON......etc


'Iron is an element, found in chemistry labs'

Pig iron:- It is iron as cast after smelting from ore. It is so called because it used to be a very simple casting made by scooping roundish depressions in a row along a runnel. Add red-hot iron, and the visual effect resembles piglets feeding from a sow. Pig iron has 5% carbon by weight or more.
Cast iron:- It is pig iron remelted (or even, these days, shipped directly to a foundry in molten form) and cast into something useful. It still has 5% or more carbon, and the carbon separates out into flakes. This reduces the tensile strength, but not the compressive strength, so it is used where compression is important. Machine tool bases are often cast iron.
Take out all but 0.25% of the carbon, add a little manganese and silicon, and you have mild steel. This is the steel that you see the most of. It works relatively easily, has good tensile and compressive strength, and is cheap. Car and appliance bodies are mild steel sheet. Coat the sheet with zinc to prevent corrosion, and use it for roofs and ducts. Most modern "wrought iron" railings are really mild steel, so you need to keep them painted. This is what most people are thinking of when the say just "steel" with no qualifiers.
Take out just about all the carbon and you have wrought iron, easy to shape on a forge and weather resistant - it rusts a lot more slowly than other steels. It is almost pure iron. Rarely seen these days.
carbon steel:-Leave in just the right amount of carbon, around 1%, and you have carbon steel. This is useful in springs, knives, and high-tensile wire rope. Its big feature is that you can change its properties from soft via springy to hard and brittle by simple heat treatment. Also sometimes called tool steel, though this tends to be used for more complex alloys.
To get stainless steel you remove the carbon and add a lot of chromium, at least 10.5%. It is capable of taking a moderately good edge, (not as good as a tool steel) but it will not rust, provided it is exposed to air so that it can form a protective oxide layer. Great for cutlery and cooking gear, but not so good for bolts, which rust out fast where you can't see them, because there is no free oxygen there.

Friday, 16 September 2016

ENGINEERING MECHANICS BY EGOR.P. POPOV

                                   INTRODUCTION 

In the world of virtuality everything is digitalised, no one bother to carry books that matches our pillows, these books are like warnings to you "hey you cant change your place while reading me" 


And everyone of us carry a electronic device capable of handling pdf,docs,xps etc files there are too many i can not mention here and as a GATE exam seeker SOM one of the vary important topic asked in this competitive examination.I am giving you what you need.

Till now we have talked about e-reading now the most popular question ever asked is "which book is best or say good for SOM" i am not just discussing about this subject it is for all but to answer the current question i am here providing you the pdf of one of the most popular books available for SOM 


(cover page)

HOW TO DOWNLOAD

It is simple as cutting a cake you just have to click on the "download your book here" and yup you will be redirected on my google drive page where again download option will appear kindly download from there IF YOU FEEL ANY PROBLEM WHILE DOWNLOADING PLEASE LEAVE A COMMENT BELOW 

REVIEW

lets review this book this book consist of point to point basis concepts means you may have to go through the texts 2-3 times but you will surely going to crystal clear your concepts.this book covers the whole syllabus with a good variety of solved and unsolved questions and it is one of the first preferred book in PU (Punjab university) syllabus so a PU student must have this book.So finalizing the review i will give this book 4 out of 5 stars which is much worth so folks give it a try and just i said you may got frustrated on the first read but be patient and keep reading .